VVerdoos
Log in
CC

cenwan cenwan

@cenwan

5 Posts0 Followers0 Following
CC
cenwan cenwan@cenwan· October 29 at 2:51 AM

CenWan Folder Gluer Maintenance Tips for Factory Teams

A Folder Gluer can deliver consistent folding and gluing only when it receives regular attention from operators and maintenance staff. Dust, paper fibers, glue residue, and worn components may gradually affect feeding accuracy, folding position, and bonding quality. Establishing a clear maintenance routine helps the machine stay stable during daily production and reduces unexpected stoppages. For packaging teams that want reliable performance and practical support, cenwanmachine provides equipment information and service guidance for factory use. Daily cleaning should begin before the machine starts and continue after the shift ends. The feeding area, folding belts, conveyor surfaces, and glue application zones need to be checked for paper dust, dried glue, or foreign objects. Clean surfaces help the sheet move smoothly and prevent uneven folding caused by accumulated residue. Operators should also inspect the feeding table and side guides to confirm that they remain free of damage and positioned correctly for the current box size. Lubrication plays an important role in keeping moving parts working properly. Chains, gears, bearings, and sliding rails should be checked according to the manufacturer guide, because insufficient lubrication can increase friction and shorten component life. Over lubrication should also be avoided, since excess oil may attract dust or stain packaging materials. A simple record of lubrication points and intervals helps the team follow the same standard across shifts. Glue system care directly affects box quality and machine cleanliness. The glue tank, nozzle, roller, and pipeline should be inspected for blockage, leakage, or dried residue. If hot melt glue is used, temperature settings should remain within the recommended range to avoid poor bonding or carbonization. Cleaning the glue path at appropriate intervals helps maintain uniform application and reduces waste caused by uneven coating. Belts and folding sections require regular inspection because they influence folding accuracy and sheet movement. Worn belts may cause slipping, while loose folding plates can create inconsistent crease positions. Operators should check belt tension, surface condition, and alignment, and replace damaged parts before they affect production. Folding tools should be adjusted carefully when changing box styles, so that each crease follows the intended line without crushing the material. Electrical and safety checks should never be ignored during maintenance. Control panels, sensors, emergency stop buttons, protective covers, and wiring connections need to remain clean, intact, and functional. Any abnormal sound, vibration, heating, or error indication should be recorded and checked before the machine continues long term operation. Keeping a maintenance log allows the team to track recurring issues and plan spare part replacement in advance. Proper maintenance does not only protect the machine; it also supports stable packaging quality and predictable output. When feeding, folding, gluing, and safety systems are checked in an organized way, the production line can run with fewer interruptions and clearer responsibility. CenWan Machine supports packaging manufacturers with folder gluer products and service information, and further details about equipment models can be found at https://www.cenwanmachine.com/product for buyers who want to match maintenance needs with suitable machine configuration.
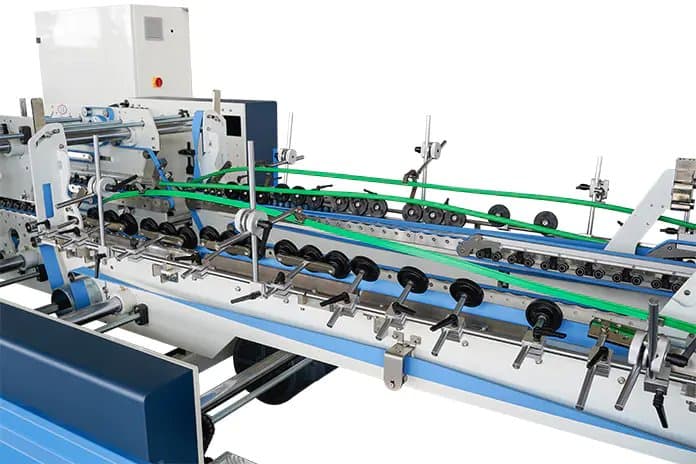
Photo shared by cenwan cenwan: A Folder Gluer can deliver consistent folding and gluing only when it receives regular attention fro
CC
cenwan cenwan@cenwan· October 22 at 5:59 AM

CenWan Box Folder Gluer Machine Dual Board Compatibility

Production managers who schedule both folding-carton and corrugated work on the same shift evaluate whether one forming platform can accept the two material families without prolonged stoppages. Units described as Box Folder Gluer Machine offered by cenwanmachine equip the infeed with variable vacuum and the folding zone with independently controlled pressure points so each blank type receives the force profile suited to its construction. The open question is whether these variable elements continue to deliver square folds and secure joints once the order stream alternates between solid board and fluted board within a single day? Solid paperboard travels as a dense continuous sheet whose scored lines respond to moderate pressure. The infeed separates successive blanks with controlled suction and advances them on belts whose speed matches the lighter mass. Side registers keep the blank centered while pre-break rollers open the scores just enough for the main folding belts to complete the form. Because the material lacks an internal air structure the compression load stays relatively uniform from edge to edge. Fluted board behaves differently. The internal air columns give the sheet greater resistance to crushing yet lower resistance to local deformation. Folding rollers therefore apply force in staged increments so the outer liners crease along the score while the flutes remain largely intact. Belt tension is raised or lowered according to flute height so the blank does not skew or collapse under its own weight during high-speed travel. These incremental adjustments keep the finished box within dimensional tolerance even when flute profiles change from one job to the next. Surface energy of the liner also dictates adhesive choice and application timing. Plain kraft accepts cold adhesive that requires a measured dwell under compression. Coated or printed liners often call for hot-melt whose open time is shorter. The adhesive station therefore switches between nozzle temperature and volumetric settings stored under different job codes. A short test run after each change confirms that the bead remains continuous and that the joint reaches handling strength before the box reaches the stacker. Changeover sequences rely on stored mechanical and electronic presets. Once an operator selects the next material grade the system recalls the corresponding vacuum level, roller gaps, belt speeds and glue parameters. Physical stops and guides are moved by servo or handwheel according to the recalled recipe, after which a handful of blanks confirm registration and fold quality. The entire sequence occupies only the time needed to clear the previous blanks and load the new stack, keeping the line productive across mixed schedules. Shared drive and frame components reduce the number of unique spare parts required. The same main motor and belt system serve both solid and fluted work; only the folding section inserts and the adhesive head tooling change when the geometry of the box style itself changes. Operators therefore learn one machine language and apply it to the full range of board types that enter the plant. Routine inspection focuses on the points of contact that experience the greatest variation in load. Vacuum cups, belt surfaces and glue nozzles are checked for wear that could affect feed reliability or bead placement. Replacement intervals are scheduled according to the proportion of corrugated versus solid board that the plant runs, so the machine remains ready for whichever material arrives next. Plants that convert both retail cartons and shipper boxes gain scheduling freedom when one platform covers the required thickness and surface spectrum. Trial runs with actual customer blanks generate records of crease accuracy, joint strength and scrap rate for each grade. Those records travel with the machine specification so purchasing teams can verify fit against the current and forecast product mix. Floor space that once held two specialized lines can instead accommodate a single versatile platform plus buffer storage. Finished boxes leave the machine in uniform stacks whether the blank began as solid paperboard or corrugated sheet. Consistent handling from infeed to exit ensures that downstream packing stations receive product of predictable size and strength. Clear documentation of the accepted board-weight range, flute profiles and coating types helps planners assign jobs without risk of overload or underperformance. Converters seeking dependable processing of both solid and fluted stocks can review the mechanical and control details of current models at the location https://www.cenwanmachine.com where Box Folder Gluer Machine offerings from cenwanmachine describe the adjustable infeed, staged folding pressures and dual-mode adhesive stations that accept successive paperboard and corrugated grades under continuous operation. Aligning a platform whose variable elements respond to density, structure and surface differences with the actual mix of orders supports uninterrupted output across varied production days.

Photo shared by cenwan cenwan: Production managers who schedule both folding-carton and corrugated work on the same shift evaluate
CC
cenwan cenwan@cenwan· October 19 at 5:16 AM

CenWan Folder Gluer Machine Waste Control Insights

Packaging operations that convert flat blanks into finished cartons encounter material loss whenever folds deviate from intended score lines or when adhesive fails to create secure bonds. Misaligned panels produce cartons that cannot close properly or that display visible defects, prompting rejection before the product reaches filling lines. Excess or insufficient glue creates similar problems by either contaminating surfaces or leaving joints weak enough to open under handling stress. Equipment designed to maintain tight registration between folding belts and to meter adhesive with repeatable volume therefore contributes directly to higher yields from each sheet of board processed. Facilities evaluating a Folder Gluer Machine available through cenwanmachine often examine whether these mechanical controls genuinely lower the volume of discarded blanks over extended runs? The folding section relies on precisely timed belts and guides that advance each blank while sequential panels are turned along pre-scored lines. When the timing remains synchronized with blank dimensions, the resulting edges meet cleanly and the carton retains square geometry. Any drift in belt speed or guide position introduces cumulative angular error that becomes visible only after the blank has progressed several stations, at which point recovery is no longer possible. Systems that monitor and correct registration in real time limit the number of blanks that travel beyond the point of useful correction. Adhesive application stations complement the folding sequence by depositing continuous or intermittent beads along designated flaps. Metering pumps and nozzle geometry determine both the volume and the placement accuracy of the glue line. Consistent bead width ensures that opposing surfaces receive sufficient coverage for bonding without overflow that would soil adjacent panels or machinery. When the adhesive remains confined to the intended zone, downstream compression sections can apply uniform pressure that sets the joint without secondary cleaning steps or rework. Changeover procedures also influence waste generation. Extended periods spent adjusting guides and timing after a size change allow operators to produce trial blanks that may later prove unusable. Mechanisms that store previous job parameters and recall them quickly reduce the number of adjustment cycles required, thereby shortening the interval during which non-conforming cartons accumulate. Operators who can verify fold and glue positions with minimal sample consumption preserve a larger proportion of the material allocated to each order. Board characteristics interact with machine settings in ways that affect final yield. Variations in caliper, moisture content, or surface coating alter how readily a blank accepts a fold or how readily adhesive wets the fiber. Equipment capable of fine adjustment to belt pressure and glue viscosity accommodates these differences without generating large quantities of test material. The ability to dial in parameters for each substrate type keeps the transition from setup to steady production brief and economical. Inspection systems mounted after the final compression section provide an additional safeguard. Optical or mechanical checks can identify cartons whose folds fall outside tolerance or whose glue lines appear incomplete, diverting them before they enter the stacking section. Early removal of defective units prevents them from mixing with acceptable product and later requiring manual sorting that consumes further labor and time. Maintenance practices sustain the precision that underpins low waste performance. Worn belts, contaminated nozzles, or loose guides gradually degrade registration and adhesive consistency. Scheduled inspection and replacement of these components keep the forming path within original design tolerances, ensuring that the machine continues to convert blanks at the same efficiency level achieved during initial commissioning. Facilities that track the ratio of finished cartons to blanks consumed gain clear visibility into the contribution of accurate folding and gluing. When the data show progressive improvement after the introduction of tighter process controls, the link between mechanical precision and material conservation becomes evident. Continued attention to these parameters supports stable output quality across successive production campaigns. Folder Gluer Machine configurations offered by cenwanmachine incorporate the registration and metering features described above, and complete equipment specifications can be reviewed at https://www.cenwanmachine.com/product where application examples and technical outlines assist evaluation of suitability for particular carton styles and production volumes.

Photo shared by cenwan cenwan: Packaging operations that convert flat blanks into finished cartons encounter material loss whenever
CC
cenwan cenwan@cenwan· August 20 at 3:53 AM

What Common Problems Cause Automatic Gluing Machine Failures According to CenWanMachine Chengwang

Operators encounter situations where an Automatic Gluing Machine and cenwanmachine unit ceases proper function during a production run, leaving adhesive application incomplete or inconsistent. Glue may fail to dispense, sensors may register false readings, or mechanical drives may stall without obvious external damage. These interruptions disrupt workflow and require methodical diagnosis to identify the source. What primary conditions most frequently produce such operational stops? Nozzle and applicator blockages rank among the frequent sources of interruption. Residual adhesive hardens inside narrow passages when temperature drops or cleaning intervals lengthen. Hot-melt systems prove especially sensitive to thermal fluctuations that allow material to solidify within the orifice. Cold-glue units face similar risks from dried residue that narrows the flow path. Regular flushing with approved solvents or thermal purging cycles clears these restrictions and restores even distribution across the substrate. Sensor and detection faults create another category of stoppage. Optical or proximity sensors that monitor board presence, glue bead continuity, or fold accuracy may accumulate dust or adhesive mist that obscures readings. Misaligned sensors generate error signals that halt the line as a protective measure. Cleaning lenses and verifying mounting positions often returns accurate detection. Calibration procedures ensure the system recognizes legitimate product flow rather than environmental interference. Pressure and pump irregularities affect adhesive delivery volume. Insufficient pressure produces gaps in the glue line, while excessive pressure causes overflow or splatter that triggers downstream sensors. Worn seals, clogged filters, or incorrect viscosity settings contribute to these imbalances. Checking pump output against manufacturer specifications and replacing degraded components stabilizes flow. Viscosity that matches the system design further supports consistent pressure across extended runs. Temperature control deviations interrupt hot-melt applications in particular. Heating elements that cycle irregularly or thermocouples that drift from calibration allow adhesive to cool below optimal fluidity or overheat into degradation. Either condition alters flow characteristics and may activate safety interlocks. Verifying heater response and sensor accuracy keeps the material within the required range. Insulation integrity around hoses and tanks also limits heat loss that would otherwise demand compensatory overheating. Mechanical alignment and drive problems introduce physical interruptions. Conveyor belts that stretch or shift cause substrates to misfeed relative to the glue head. Timing chains or gears that wear alter the synchronization between product movement and adhesive application. Visual inspection of belt tracking and tension, followed by adjustment or replacement of worn elements, restores coordinated motion. Lubrication schedules for moving parts reduce friction that accelerates such wear. Electrical and control system anomalies complete the range of common causes. Loose connections, voltage fluctuations, or software parameter drift can freeze the sequence logic. Error codes displayed on the interface provide directional clues toward the affected circuit or module. Systematic testing of power supply stability and input-output signals isolates the fault. Restoring factory-default parameters after hardware correction frequently clears residual software conflicts. After examining nozzle condition, sensor clarity, pressure stability, temperature accuracy, mechanical alignment, and electrical integrity the pathways to resumed operation become defined. Many interruptions trace to cumulative effects of routine wear or overlooked cleaning rather than sudden component failure. Facilities seeking equipment designed with accessible maintenance points and stable process controls may review current models at https://www.cenwanmachine.com where Chengwang production incorporates Automatic Gluing Machine and cenwanmachine considerations for sustained line performance.

Photo shared by cenwan cenwan: Operators encounter situations where an Automatic Gluing Machine and cenwanmachine unit ceases prope